


AccuLock™ R Consumables
Tregaskiss® AccuLock™ R consumables virtually eliminate contact tip cross-threading and extend tip life, so robotic and automatic cells spend less time down and more time welding.
Overview
Less downtime. Less troubleshooting.
Tregaskiss® AccuLock™ R consumables are built to reduce the planned and unplanned downtime that comes with frequent consumable changes in robotic welding. Each contact tip has a long tail that concentrically aligns inside the diffuser before the coarse threads engage, making it virtually impossible to cross-thread. With 60% of the tip buried in the diffuser, away from the heat of the weld, tips last longer and need replacing less often, and mating tapers at the tip and diffuser provide excellent electrical conductivity. For pulse welding, AccuLock HDP contact tips can last up to 10x longer than copper, depending on the application. Upgrading is low effort and low risk: in most cases, your current tip and diffuser can be replaced with no impact to Tool Center Point (TCP). QUICK LOAD® liners reload from the front in less than half the time of rear-load liners. And because AccuLock R shares a common contact tip with Bernard® AccuLock S consumables, shops running robotic, automatic, and semi-automatic guns can simplify inventory and cut costs.
Specifications
| Compatible guns | Atlas™, TA3, CA3, 600 Amp robotic water-cooled, MA1, MW1, Bernard® T-Gun™ and W-Gun™ semi-automatic water-cooled guns |
|---|---|
| Wire sizes | 0.030″–3/32″ (0.8–2.4 mm) |
| System components | Contact tips, gas diffusers, nozzles, QUICK LOAD® liners |
| Diffuser styles | Slip-on and thread-on |
| Contact tips | HD copper, HD copper aluminum-specific, HD chrome zirconium, HDP; all 0.350″ O.D. |
| Nozzle bore | 5/8″ |
| Applications | Automotive, general manufacturing & fabrication, heavy equipment |
Consumables
CONSUMABLES
Contact Tips
AccuLock HD Contact Tips; Copper
All AccuLock contact tips are 0.350″ O.D. Torque to 30 in.-lbs. (3.5 Nm).
| Part Number | Description |
|---|---|
| T-A030CH | 0.030″ (0.8 mm); qty. 10 |
| T-A030CH-100 | 0.030″ (0.8 mm); qty. 100 |
| T-A030CH-1000 | 0.030″ (0.8 mm); qty. 1000 |
| T-A035CH | 0.035″ (0.9 mm); qty. 10 |
| T-A035CH-100 | 0.035″ (0.9 mm); qty. 100 |
| T-A035CH-1000 | 0.035″ (0.9 mm); qty. 1000 |
| T-A039CH | 0.039″ (1.0 mm); qty. 10 |
| T-A039CH-100 | 0.039″ (1.0 mm); qty. 100 |
| T-A039CH-1000 | 0.039″ (1.0 mm); qty. 1000 |
| T-A045CH | 0.045″ (1.2 mm); qty. 10 |
| T-A045CH-100 | 0.045″ (1.2 mm); qty. 100 |
| T-A045CH-1000 | 0.045″ (1.2 mm); qty. 1000 |
| T-A052CH | 0.052″ (1.3 mm); qty. 10 |
| T-A052CH-100 | 0.052″ (1.3 mm); qty. 100 |
| T-A052CH-1000 | 0.052″ (1.3 mm); qty. 1000 |
| T-A062CH | 1/16″ (1.6 mm); qty. 10 |
| T-A062CH-100 | 1/16″ (1.6 mm); qty. 100 |
| T-A072CH | 0.072″ (1.8 mm); qty. 10 |
| T-A072CH-100 | 0.072″ (1.8 mm); qty. 100 |
| T-A078CH | 5/64″ (2.0 mm); qty. 10 |
| T-A078CH-100 | 5/64″ (2.0 mm); qty. 100 |
| T-A094CH | 3/32″ (2.4 mm); qty. 10 |
| T-A094CH-100 | 3/32″ (2.4 mm); qty. 100 |
AccuLock HD Contact Tips; Copper, Aluminum-Specific
| Part Number | Description |
|---|---|
| T-A035AL | 0.035″ (0.9 mm); qty. 10 |
| T-A035AL-100 | 0.035″ (0.9 mm); qty. 100 |
| T-A047AL | 3/64″ (1.2 mm); qty. 10 |
| T-A047AL-100 | 3/64″ (1.2 mm); qty. 100 |
| T-A062AL | 1/16″ (1.6 mm); qty. 10 |
| T-A062AL-100 | 1/16″ (1.6 mm); qty. 100 |
AccuLock HD Contact Tips; Chrome Zirconium
| Part Number | Description |
|---|---|
| T-A030ZH | 0.030″ (0.8 mm); qty. 10 |
| T-A030ZH-100 | 0.030″ (0.8 mm); qty. 100 |
| T-A035ZH | 0.035″ (0.9 mm); qty. 10 |
| T-A035ZH-100 | 0.035″ (0.9 mm); qty. 100 |
| T-A039ZH | 0.039″ (1.0 mm); qty. 10 |
| T-A039ZH-100 | 0.039″ (1.0 mm); qty. 100 |
| T-A045ZH | 0.045″ (1.2 mm); qty. 10 |
| T-A045ZH-100 | 0.045″ (1.2 mm); qty. 100 |
| T-A052ZH | 0.052″ (1.3 mm); qty. 10 |
| T-A052ZH-100 | 0.052″ (1.3 mm); qty. 100 |
| T-A062ZH | 1/16″ (1.6 mm); qty. 10 |
| T-A062ZH-100 | 1/16″ (1.6 mm); qty. 100 |
AccuLock HDP Contact Tips
Made from a special alloy that resists arc erosion and wear, HDP tips can last up to 10x longer than copper and chrome zirconium tips in pulse welding, depending on the application, with improved arc stability and reduced spatter.
| Part Number | Description |
|---|---|
| T-A035WH | 0.035″ (0.9 mm); qty. 10 |
| T-A035WH-100 | 0.035″ (0.9 mm); qty. 100 |
| T-A039WH | 0.039″ (1.0 mm); qty. 10 |
| T-A039WH-100 | 0.039″ (1.0 mm); qty. 100 |
| T-A045WH | 0.045″ (1.2 mm); qty. 10 |
| T-A045WH-100 | 0.045″ (1.2 mm); qty. 100 |
| T-A052WH | 0.052″ (1.3 mm); qty. 10 |
| T-A052WH-100 | 0.052″ (1.3 mm); qty. 100 |
AccuLock Tip Tool
| Part Number | Description |
|---|---|
| T-ALTOOL | AccuLock tip tool; qty. 1 |
Gas Diffusers
| Part Number | Description |
|---|---|
| D-ATSH | Slip-on; for TOUGH GUN® TA3 and CA3, MA1, 500 A MW1, Auto Head, and 400 A T-Gun™ (compact); qty. 10 |
| D-ATSH-100 | Slip-on; qty. 100 |
| D-ATTH | Thread-on; for TOUGH GUN® TA3 and CA3, MA1, 500 A MW1, Auto Head, 400 A T-Gun™ (compact) and 450 A T-Gun™; qty. 10 |
| D-ATTH-100 | Thread-on; qty. 100 |
| D-ATTH-RW1 | Thread-on; for 600 A robotic water-cooled guns; qty. 25 |
| D-ATTH-MW1 | Thread-on; for 600 A MW1 and 600 A T-Gun™; qty. 25 |
| D-ATSH-AW2 | Slip-on; for AW2 and 600 A W-Gun™; qty. 25 |
Nozzles; Slip-On (5/8″ bore)
| Part Number | Description |
|---|---|
| 401-6-62 | 1/8″ recess, tapered, copper, 1.062″ O.D.; qty. 10 |
| 401-4-62 | 1/8″ recess, tapered, copper, 0.938″ O.D.; qty. 10 |
| 401-5-62 | 1/4″ recess, tapered, copper, 1.062″ O.D.; qty. 10 |
| 401-8-62 | 1/8″ stick-out, tapered, copper, 0.938″ O.D.; qty. 10 |
| 401-81-62 | 1/8″ stick-out, tapered, copper, 1.062″ O.D.; qty. 10 |
| 401-48-62 | Flush, bottleneck, copper, 1.062″ O.D.; qty. 10 |
| 401-7-62 | 1/4″ recess, tapered, brass, 1.106″ O.D.; qty. 10 |
| 401-71-62 | 1/8″ recess, tapered, brass, 1.106″ O.D.; qty. 10 |
| 401-87-62 | 1/8″ stick-out, tapered, brass, 1.062″ O.D.; qty. 10 |
| 401-30-62 | 1/8″ stick-out, bottleneck, brass, 0.938″ O.D.; qty. 10 |
| 401-9-75 | 3/4″ bore, 1/2″ recess, tapered, copper, 1.062″ O.D.; for Miller® HD MIG process; qty. 10 |
Nozzles; Thread-On (5/8″ bore)
| Part Number | Description |
|---|---|
| 401-14-62 | 1/8″ recess, tapered, copper, 1.062″ O.D.; qty. 10 |
| 401-43-62 | 1/8″ recess, tapered, copper, 0.938″ O.D.; qty. 10 |
| 401-18-62 | 1/8″ stick-out, tapered, copper, 0.938″ O.D.; qty. 10 |
| 401-20-62 | 1/8″ stick-out, tapered, copper, 1.062″ O.D.; qty. 10 |
| 401-30-62T | 1/8″ stick-out, bottleneck, brass, 0.938″ O.D.; qty. 10 |
All nozzles use the RCT-01 reamer cutter blade, except 401-9-75 (RCT-13).
Teach Pointers (for robotic programming)
| Part Number | Description |
|---|---|
| T-A001TP | Adjustable; qty. 1 |
| T-A050TP | 1/2″; qty. 1 |
| T-A062TP | 5/8″; qty. 1 |
| T-A075TP | 3/4″; qty. 1 |
| T-A10MTP | 10 mm; qty. 1 |
| T-A15MTP | 15 mm; qty. 1 |
QUICK LOAD® Liners
| Part Number | Description |
|---|---|
| 415-35-6Q | 0.035″–0.045″ (0.9–1.2 mm); 6′ (1.8 m) |
| 415-35-10Q | 0.035″–0.045″ (0.9–1.2 mm); 10′ (3.05 m) |
| 415-35-15Q | 0.035″–0.045″ (0.9–1.2 mm); 15′ (4.6 m) |
| 415-35-25Q | 0.035″–0.045″ (0.9–1.2 mm); 25′ (7.6 m) |
| 415-116-6Q | 0.045″–1/16″ (1.2–1.6 mm); 6′ (1.8 m) |
| 415-116-10Q | 0.045″–1/16″ (1.2–1.6 mm); 10′ (3.05 m) |
| 415-116-15Q | 0.045″–1/16″ (1.2–1.6 mm); 15′ (4.6 m) |
| 415-116-25Q | 0.045″–1/16″ (1.2–1.6 mm); 25′ (7.6 m) |
QUICK LOAD® E-Z Feed™ Liners
| Part Number | Description |
|---|---|
| 415-35-062Q | 0.035″–0.045″ (0.9–1.2 mm); 6′ (1.8 m); galvanized; requires 415-26 retainer |
| 415-116-062Q | 0.045″–1/16″ (1.2–1.6 mm); 6′ (1.8 m); galvanized; includes 415-31 retainer |
QUICK LOAD® Liner Retainers (required for initial installation, sold separately)
| Part Number | Description |
|---|---|
| 415-26 | 0.030″–5/64″ (0.8–2.0 mm); for Tregaskiss® TOUGH GUN® robotic and automatic guns, and Bernard® BTB, TGX™, and Clean Air™ guns |
| 415-37 | 0.030″–5/64″ (0.8–2.0 mm); for most Tweco® MIG guns |
| 415-31 | 0.045″–1/16″ (1.2–1.6 mm); required for 415-116-062Q |
Resources & documentation
No documents in this language yet.
Videos, guides & customer stories
 Videos
Keep It Genuine.
Case Study
 Videos
Welding Students in Tulsa Benefit from Bernard® MIG Guns and Consumables
Case Study
 Videos
Bernard® & AccuLock™ Drive Productivity at East Lake Mfg.
Case Study
 Videos
Vactor’s Formula for Better Welding
Case Study
 Videos
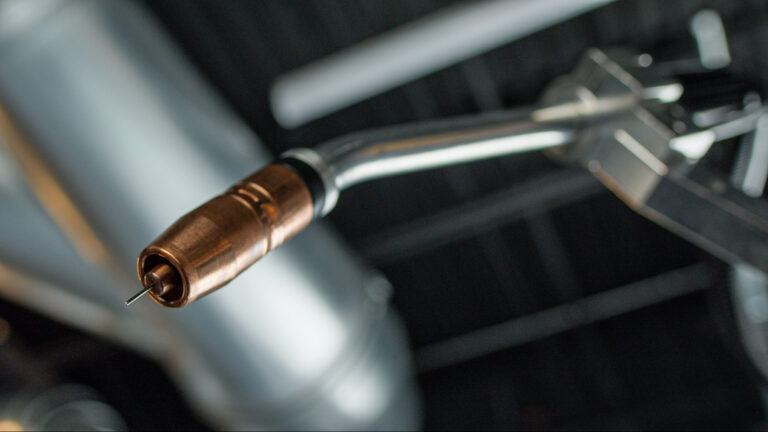
Video | How to change AccuLock R Consumables on a robotic MIG gun
Front-End Consumable
 Videos
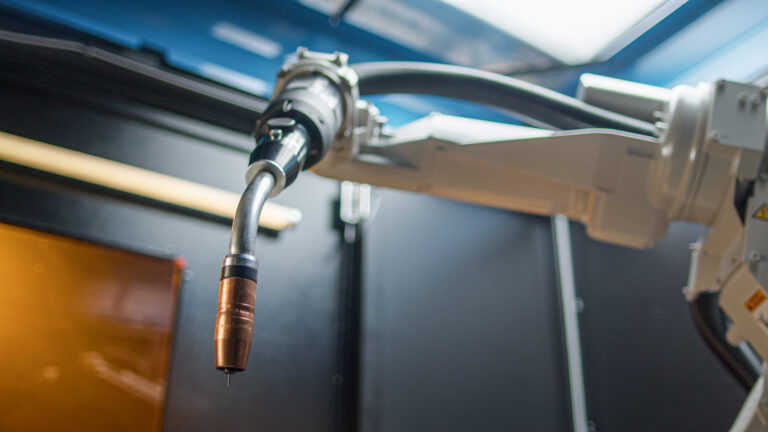
Video | How to convert TOUGH LOCK to AccuLock R Consumables on a robotic MIG gun
 Videos
Video | How to convert TOUGH LOCK to AccuLock R Consumables for BTB MIG guns
Nothing here yet.
Buy through an authorized distributor